

Office and Hotel Raised Floor Solution
| Application | Configuration principle |
|---|---|
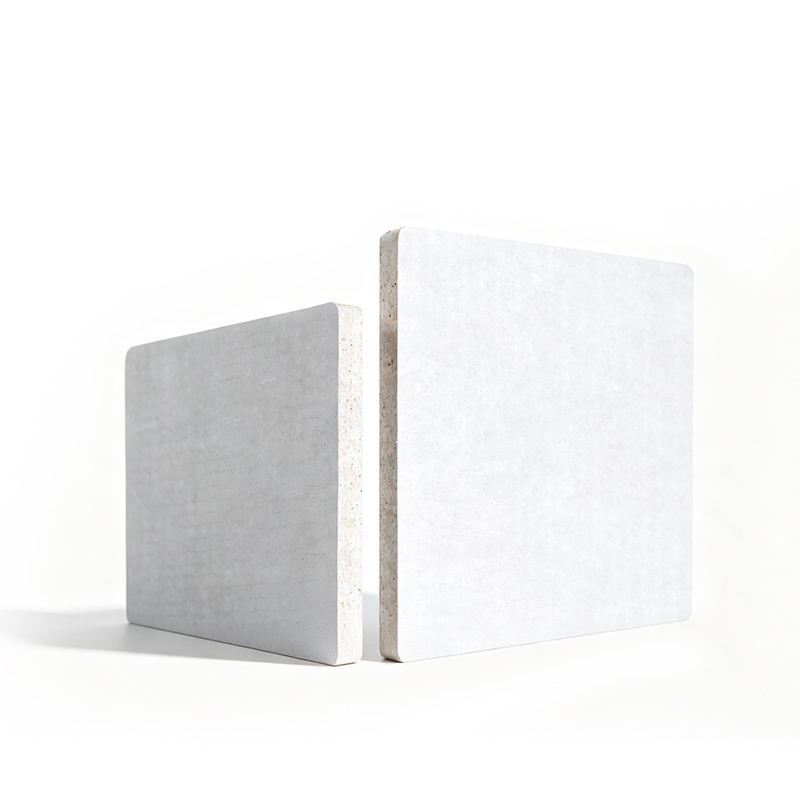
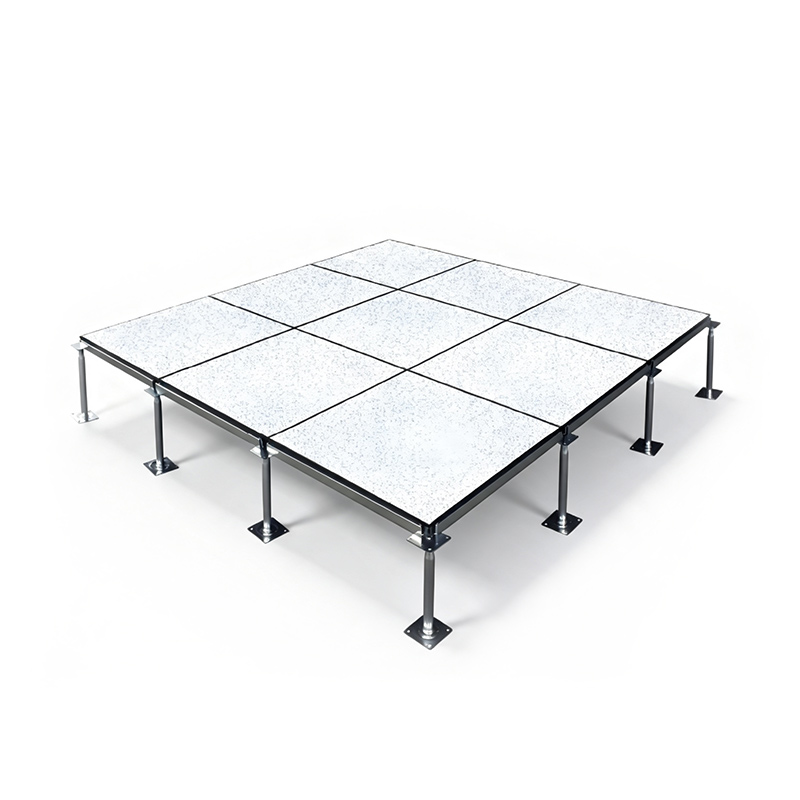
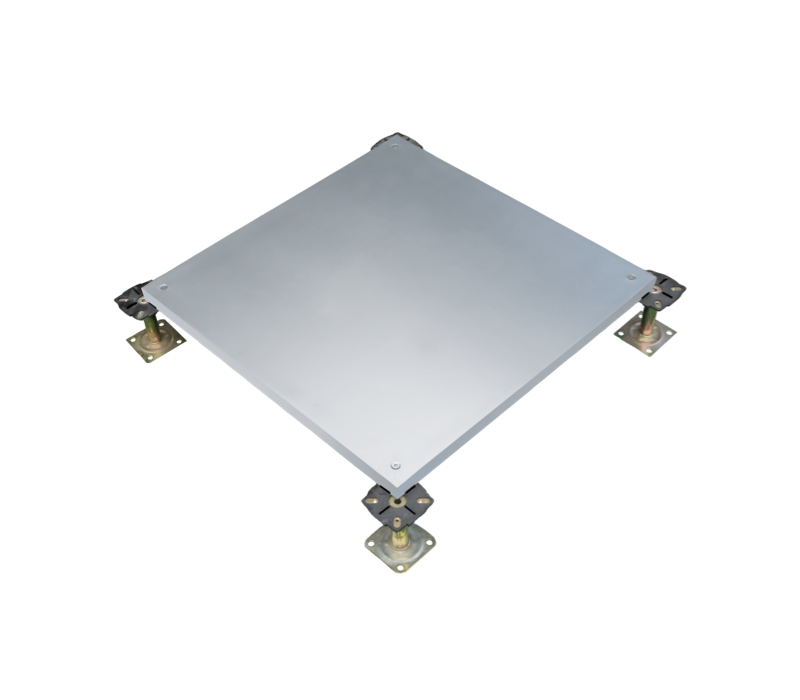
| Massif UV raised floor | An upgraded OA network floor with lighter panels for cable routing and maintenance in offices, hotels and commercial spaces. |
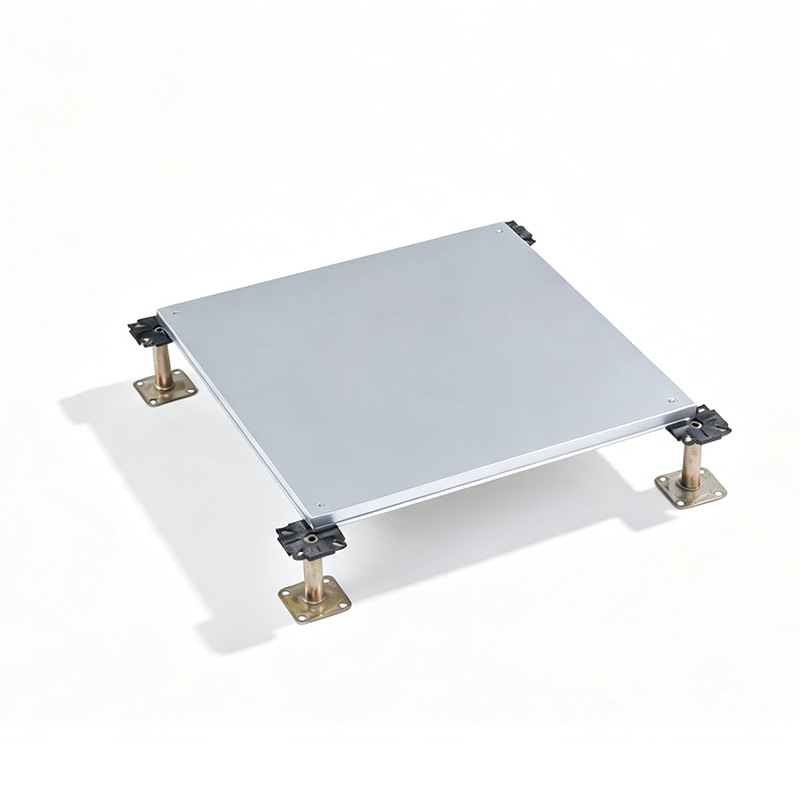
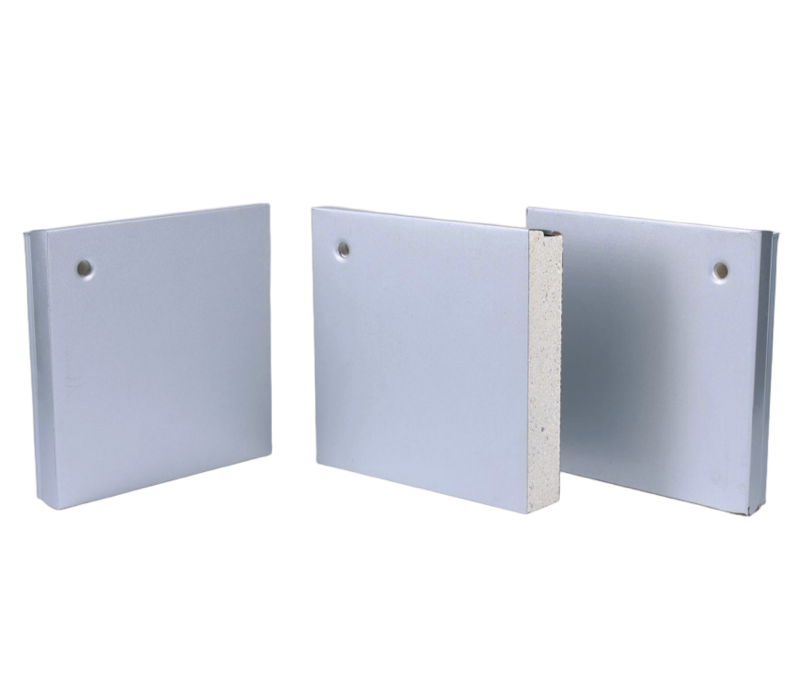
| Upgraded six-sided steel raised floor | A lightweight inorganic core encapsulated on all six sides by galvanized steel, lighter than traditional six-sided steel panels while retaining protected edges and removability. |
| Finish and height configuration | Confirm against carpet, PVC or other office finishes, raised height, service locations and access frequency. |
This solution is intended for owners, design and procurement teams, flooring contractors and distributors serving offices, hotels, showrooms and commercial public spaces.
It is not an anti-static equipment-room solution. Projects requiring ESD control and grounding should use a dedicated anti-static raised-floor system.
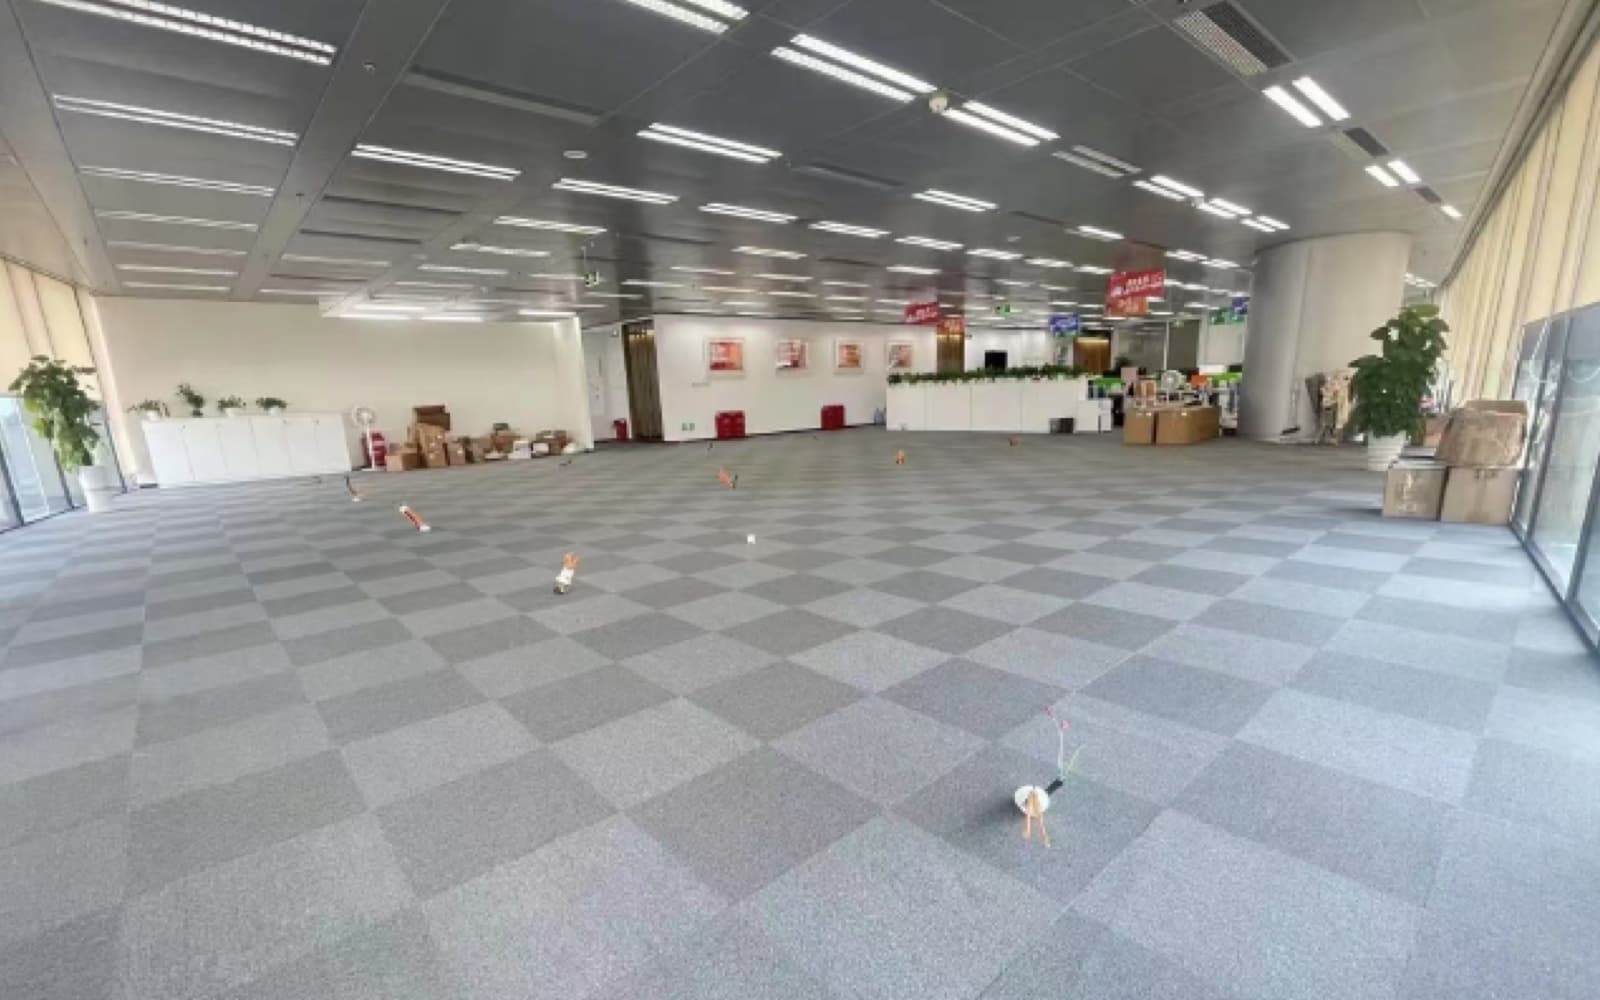
Is the upgraded OA network floor or upgraded six-sided steel floor more suitable?
How should floor height, loading and finish coordinate with the space?
Where is the boundary between ordinary and anti-static raised flooring?
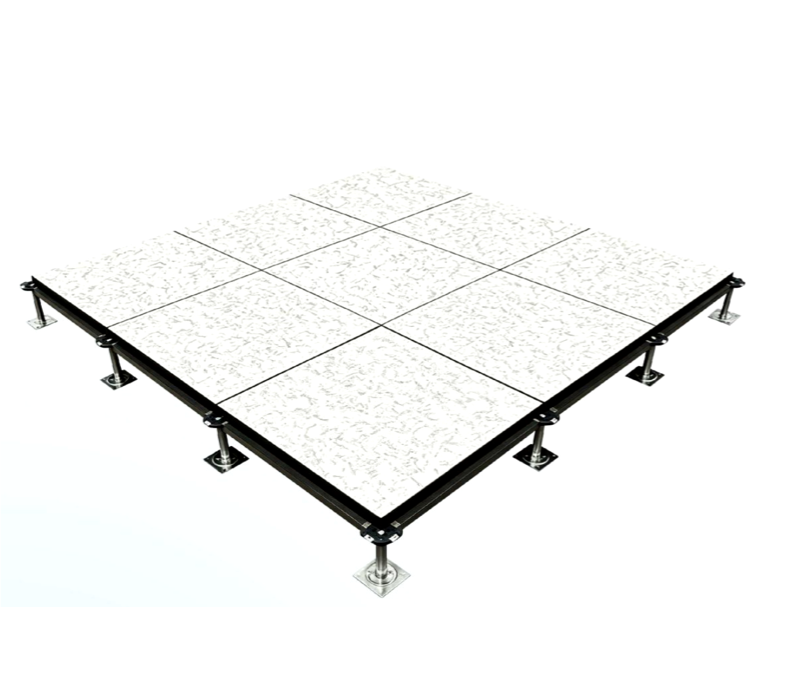
Adjustable Pedestal System
Creates orderly underfloor void for efficient cable routing, local access, and precise floor-level adjustment.
Lightweight Panel Design
Upgraded configurations feature lighter panels to reduce logistics costs and simplify on-site handling.
Non-Anti-Static Standard Configuration
Ordinary office and hotel raised flooring is not an anti-static system; verify requirements for sensitive environments.
Performance Parameters
Load capacity must correspond to specific panel model, pedestal height, and defined test conditions; heavy-load areas require separate confirmation.
Office, hotel or commercial-space use
Finished floor level, raised height and cable capacity
Panel model, finish, access frequency and maintenance method
Concentrated load, rolling load, furniture layout and local heavy-load positions
Test reports, certificates and production evidence shown externally should correspond to the actual product model, specification and test conditions. This solution page provides basic evidence and does not use unrelated certificates to infer complete-system performance.
With the currently available materials, evidence of real production, finished-product inspection and principal certificates is sufficient. Detailed test data can remain on the relevant product or quality-certification page.